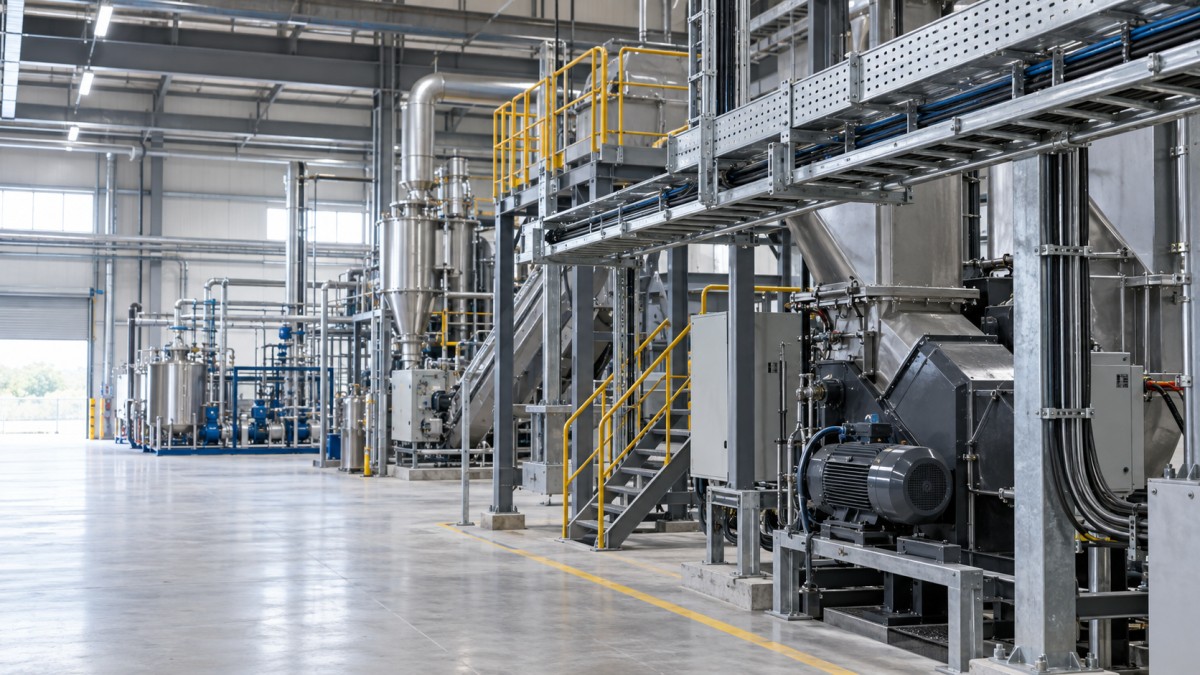
Battery recycling projects are moving from simple collection and dismantling toward integrated facilities that can discharge, shred, separate, refine, and recover valuable materials. For cable tray designers and buyers, this is not one uniform production area. A receiving hall, enclosed mechanical treatment line, black mass handling zone, hydrometallurgical process area, utility plant, laboratory, warehouse, and electrical room can place very different demands on the cable support system.
The practical challenge is to keep power, control, instrumentation, fire and gas, communications, and safety circuits organized while controlling contamination, corrosion, access, and future process changes. Selecting a tray only by width and material name can leave major gaps in the purchase scope. EPC teams should define the system by area, cable function, exposure, support condition, and installation sequence before requesting quotations.
Why Battery Recycling Plants Need Zone-Based Planning
Battery recycling can combine logistics operations, dusty mechanical processing, chemical handling, water treatment, ventilation, and high electrical loads within one site. Cable routes may pass from dry administrative or electrical spaces into washdown areas, enclosed process lines, outdoor pipe racks, and zones controlled by the project fire or hazardous-area design. A finish that is adequate in a switch room may be unsuitable close to wet chemical equipment, while a covered tray that protects against falling debris may retain contamination or moisture elsewhere.
Zone-based planning starts with the plant layout and process description. Each route should be assigned an environmental condition, cable group, cleaning method, access requirement, and expected expansion demand. The route schedule can then connect those conditions to tray type, material, support arrangement, covers, dividers, and fittings. This is more reliable than applying one cable tray specification across the whole facility.
The design should also recognize that the battery feedstock and process technology may change over the facility life. New chemistries, additional separation stages, or a refining expansion can add motors, instruments, analyzers, and ventilation equipment. Accessible routes and planned spare capacity make these changes easier without encouraging uncontrolled cable additions.
Match Cable Tray Type to Process Function
Main Power Routes
Ladder cable tray is often considered for main feeders serving shredders, separators, ventilation systems, pumps, compressors, and refining equipment. Its open construction supports cable ventilation, inspection, and entry or exit. The selection must still be checked against the cable load, support span, fitting arrangement, pulling forces, and project-required structural evidence. Sheet thickness alone does not establish system capacity.
Control and Instrumentation Routes
Perforated cable tray can provide continuous support for smaller control and instrumentation cables. It may be suitable around process skids where frequent branches are needed, provided the material, drainage, ventilation, and cleaning requirements are addressed. Wire mesh tray can be useful in clean, accessible indoor areas with frequent low-voltage drops, but it should not be assumed suitable for dusty, corrosive, or high-mechanical-risk zones.
Protected Local Circuits
Cable trunking or covered trough systems may protect selected local circuits from falling particles or accidental contact. However, a cover changes access, heat dissipation, cleaning, and drainage. Covers should therefore be specified by route and exposure, together with compatible clamps and removal clearance. Fully enclosing every route can make inspection and contamination control more difficult.
Translate Plant Areas into Procurement Requirements
| Plant Area | Routing Conditions | Cable Tray Buying Focus |
|---|---|---|
| Receiving and discharge | Material movement, vehicle interfaces, inspection equipment, possible future line changes | Mechanical protection, elevated routes, accessible branches, robust supports, route identification |
| Mechanical processing | Dense motors and sensors, enclosed equipment, dust-control ducting, vibration | Power and control separation, short-radius branches where approved, vibration-resistant hardware, cleaning access |
| Black mass handling | Fine-material containment, extraction systems, restricted cleaning practices | Contamination control, suitable covers where required, smooth accessible surfaces, project-approved materials |
| Wet refining and utilities | Chemical exposure, washdown, condensation, piping congestion, outdoor transitions | Corrosion assessment, drainage, material compatibility, support finish, fasteners and coating repair |
| Electrical rooms and laboratories | Clean indoor routing, frequent low-voltage distribution, controlled access | Neat branch management, usable dimensions, trunking transitions, spare capacity, coordinated elevations |
This area schedule should be linked to drawings and quantities. If a route crosses two exposure zones, the transition point and material interface need a defined detail. Buyers should avoid leaving field crews to decide where a finish changes or how incompatible tray profiles connect.
Control Corrosion, Contamination, and Fire Interfaces
Material selection depends on the actual process environment. Hot-dip galvanized steel may be practical in many dry industrial and outdoor areas when the project exposure and specification permit it. Stainless steel or another approved corrosion-resistant system may be required near aggressive wet-process zones. Pre-galvanized products may suit controlled indoor areas but should not be treated as equivalent to fabrication followed by hot-dip galvanizing.
Tray body, fittings, supports, splice plates, covers, clamps, fasteners, and bonding components should be evaluated together. Dissimilar metals, cut edges, field-drilled holes, damaged coatings, and water traps can become local weak points. The purchase specification should identify permitted materials, repair procedures, cleaning limitations, and whether supports are included in the same corrosion system.
Battery recycling also requires close coordination with the project's fire, gas detection, ventilation, and hazardous-area design. Cable tray is a support system; it does not by itself make cables or equipment suitable for a classified area. Cable type, separation, fire barriers, penetration sealing, emergency routing, bonding, and equipment selection must follow the approved electrical and safety design. Tray covers should not be promoted as a universal fire-protection solution.
Coordinate Process Skids, Supports, and Expansion
Recycling plants often combine vendor skids from different process specialists. Each skid can arrive with its own local tray, cable entry points, and support assumptions. Even products with the same nominal width may use different side-rail shapes, hole patterns, fitting radii, or finishes. Battery-limit drawings should identify tray elevation, direction, usable dimensions, cable load, material, connection hardware, and responsibility for the first external support.
Main routes should preserve access to equipment doors, ventilation filters, sampling points, valves, platforms, and maintenance lifting paths. Supports must be coordinated with structural steel and process piping rather than attached wherever space remains. Where vibration is expected, the support and fastening strategy should be reviewed by the responsible engineer, including any need for flexible cable transitions.
Expansion planning should identify reserved routes and branch locations instead of distributing empty space randomly. Future circuits still require support capacity, bend space, segregation, and accessible pulling paths. Removable sections or planned crossing points can reduce later disruption around operating equipment.
RFQ Checklist and Final Buying Advice
- Issue route drawings, cable schedules, process-area descriptions, support assumptions, and project safety classifications.
- Define tray type, usable width, side-rail height, straight length, rung spacing, fitting radius, material, and finish by area.
- List bends, tees, reducers, risers, crosses, covers, dividers, drop-outs, splice plates, clamps, fasteners, and bonding accessories.
- Confirm cleaning, drainage, contamination-control, and coating-repair requirements for each exposure zone.
- Review every skid interface and identify responsibility for transition fittings and local supports.
- Request the project-required structural, material, test, dimensional, and inspection documents before production.
- Pack and label materials by installation area so fittings and accessories arrive with their corresponding straight sections.
A reliable cable tray package for battery recycling is built around process zones and interfaces, not one generic catalogue selection. Procurement teams should establish environmental conditions, cable functions, support responsibilities, and future changes before comparing prices. That approach reduces incompatible parts, uncontrolled field fabrication, and maintenance problems after commissioning.
HONGFENG / Cable Tray Pro can review route schedules, material options, fittings, support requirements, skid interfaces, and export packing for battery recycling and other industrial projects. Share the available drawings and procurement specification to discuss a practical cable tray package for each plant area.
Navigation
Send Us A Message
Get in touch with us
Phone